Company & Capabilities

An overview of our development expertise, manufacturing infrastructure, and technical capabilities.

Reactor-Image-for-Website-01_result.webp

MM Herbs is a research-driven manufacturer and CDMO with integrated capabilities spanning process development, scale-up, and commercial manufacturing. Established in 2017, the company was built to bridge the gap between laboratory development and scalable, reliable manufacturing.

Supported by ISO-certified quality management systems, we operate as an integrated development and manufacturing partner, combining strong process understanding, scale-up expertise, and commercial production on a single platform to support customers across different stages of the product lifecycle with a focus on quality, consistency, and long-term supply.

Operating Model

MM Herbs operates as a Contract Development and Manufacturing Organisation (CDMO), integrating research, process development, and manufacturing within a structured operating model.

Our engagement typically spans:

  • Process development and route optimisation

  • Pilot-scale validation and scale-up

  • Commercial manufacturing and long-term supply

This integrated approach enables smooth technology transfer, reduced development risk, and consistent execution from development through commercialisation.

Reactor-Image-for-Website-03_result.webp

Facilities & Infrastructure

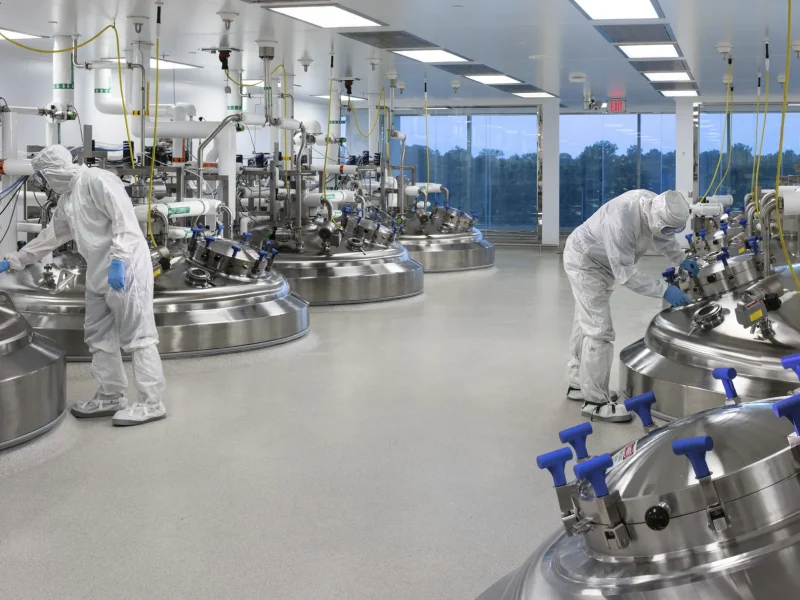
Our capabilities are supported by dedicated R&D and manufacturing infrastructure designed to address multi-chemistry, multi-product, and scalable manufacturing requirements across different stages of development and commercialization.

Research & Development Centre

Our R&D and process development activities are supported by a dedicated centre located in Bengaluru, focused on process development, optimisation, and reliable scale-up.

Key Capabilities

  • Well-equipped laboratories for process and product development
  • Pilot-scale facilities supporting scale-up and process validation
  • Route scouting, process optimisation, and impurity profiling
  • Close coordination between R&D, production, and quality teams to ensure effective technology transfer

The R&D centre plays a critical role in translating laboratory development into robust, scalable, and commercially viable manufacturing processes.

Manufacturing Facility

Our manufacturing facility is located in the KIADB Industrial Area, Mysuru, and is designed to support safe, flexible, and efficient multi-product operations across diverse chemistries.

Facility Highlights

  • Approximately 2 acres of industrial land with ~10,000 sq. ft. of built-up production area
  • Six dedicated production blocks enabling parallel manufacturing
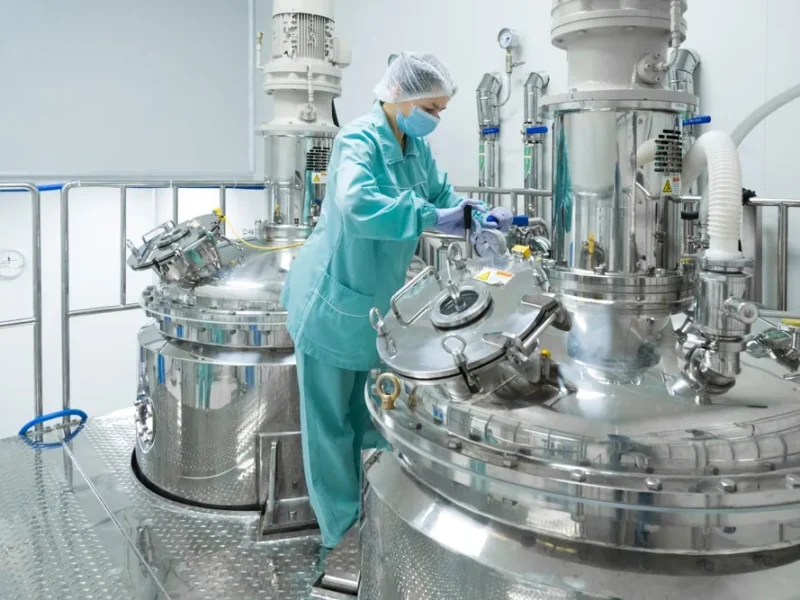
  • Reactor capacities ranging from 50 L to 8,000 L
  • Reactors constructed in glass-lined, graphite, and stainless steel materials
  • Installed manufacturing capacity of approximately 100 KL

The plant layout supports controlled material flow, effective segregation of operations, and consistent adherence to safety and quality requirements.

Aromatics & Nutraceutical Processing Capabilities

Our infrastructure also supports the development and manufacture of aromatics and nutraceutical ingredients, with controlled processing conditions, standardised operating parameters, and a strong focus on batch-to-batch consistency.

Facilities and systems are designed to support aroma-related applications and nutraceutical products while maintaining consistent quality, operational safety, and supply reliability.

Utilities, Storage & Material Handling

The manufacturing facility is supported by utilities, storage, and material handling infrastructure required for controlled and compliant operations.

  • Cold storage facility (~150 cu. m.) for finished product storage
  • Dedicated areas for quarantined, approved, and rejected materials
  • Utilities designed to support a wide range of reaction conditions
  • Structured material handling systems to ensure traceability and product integrity

These capabilities are supported by strong process understanding, safety assessments, and scalability considerations to ensure reliable transition from development to commercial manufacturing.

Reaction Capabilities

  • Grignard reaction
  • Friedel-Craft’s Reaction
  • Halogenation Reactions
  • Nitration, POCl3, Thionyl Chloride etc reactions
  • C-C bond reactions
  • High Temperature reactions (220 °C to 240 °C)
  • Low Temperature Reactions ( Up to -78 °C)
  • Highly Acidic Reactions
  • Chiral Synthesis
  • C-H activation reactions
  • Multi Step Synthesis of Complex Molecules/Targets
  • Challenging chemistry
  • High Vacuum Distillation
  • Hetero bond forming reactions

How We Support Our Customers

We believe there are no limits to what science can do. Research and development are the heart and soul of everything we do at Ganapa Life Science. We are a unique specialty chemical manufacturing company who specialize in high quality, affordable and innovative solutions in drug research.

bullseye
Our Area of Focus

Discovery, development, and supply of specialty products and advanced molecules for CRAMS and CDMO programs across pharmaceuticals, nutraceuticals, and aromatics.

development
Development

Continuous improvement driven by scientific rigor, ensuring processes and procedures remain current, efficient, and execution-ready.

high-quality
Quality

Quality is embedded across development and manufacturing, supported by ISO-certified systems, documented controls, and robust compliance practices.

research
Research & Development

A scientist-led R&D team focused on new product development and process improvement, enabling efficient translation from concept to scalable processes.

iteration
Process Development

Expertise in process development, optimization, and scale-up from laboratory to commercial production, with emphasis on safety, efficiency, and reliability.

capability
Analytical Capability

Comprehensive analytical support for R&D and manufacturing, including in-process controls, final release testing, and stability studies aligned with ICH guidelines.